The most common pitfall in mold selection: customers only compare mold quotations, see the hot runner is more expensive, and directly choose the cold runner. But many overlook a hidden cost: runner scrap.
Cold runners have low upfront investment, but every injection cycle produces runner scrap. Even if ground and reused, there is material downgrading, loss, sorting labor, and warehousing cost; especially for high-priced engineering plastics like PC and POM, the depreciation loss of runner scrap is astonishing.
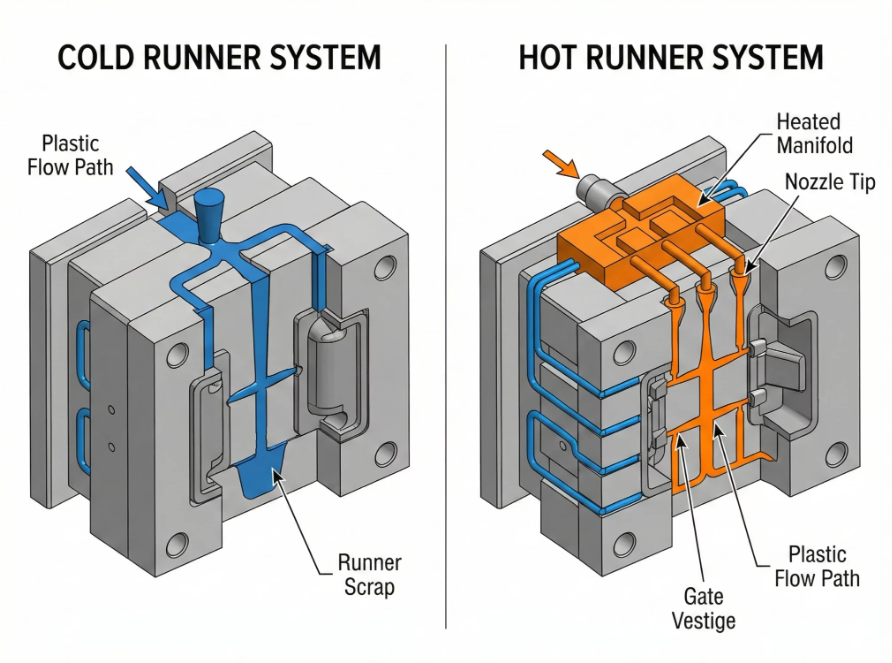
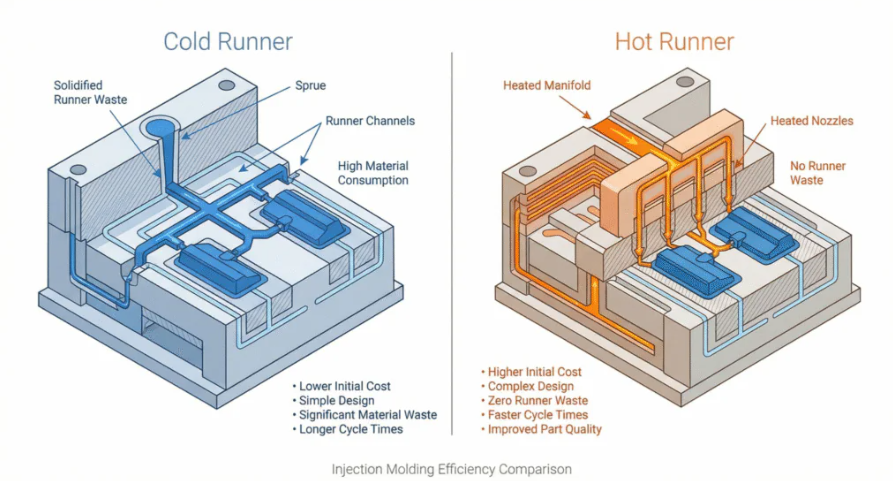
Hot runners keep the plastic in the runner continuously molten, with almost no runner waste, shorter molding cycles, and better automation compatibility — but higher upfront mold investment.
There is no absolute good or bad between cold and hot runners. The core is to calculate the break-even point clearly: below 100,000 pieces per year, cold runner total cost is lower; above 500,000 pieces per year, the material savings from a hot runner are enough to cover the extra mold investment.
Cold Runner
No heating in the runner. After the plastic fills the cavity, the runner and product cool and solidify together. After mold opening, the runner must be separated, then ground and blended back.
✅ Simple mold, low initial cost, easy maintenance, convenient color and material changes.
❌ Runner waste; slower cooling, longer cycle; grinding, sorting, and warehousing labor; recycled material performance degrades.
Hot Runner
Hot runner manifold, heated nozzles, and temperature controller are added. The runner stays at constant temperature and the plastic remains molten, with no large runner scrap.
✅ Material utilization near 100%; cycle shortened by 15%~25%; high automation; small gate marks, stable dimensions.
❌ Higher mold cost; complex structure, regular maintenance required; time-consuming purging during frequent color or material changes.
Core Formula
Break-even output = Extra investment in hot runner mold ÷ Comprehensive savings per piece (material + labor + machine cycle benefits)
Reference Scenario:
Annual output < 100,000 pieces: Prioritize cold runner. Total runner scrap loss is limited; the extra hot runner investment is hard to recover.
Annual output 100,000–500,000 pieces: Evaluation range. For ordinary materials (ABS, PP), continue with cold runner; for high-priced engineering materials (PC, POM, PA+GF), calculate separately.
Annual output > 500,000 pieces: Prioritize hot runner. Combined savings from runner scrap depreciation, labor, and machine efficiency make long-term total cost lower.
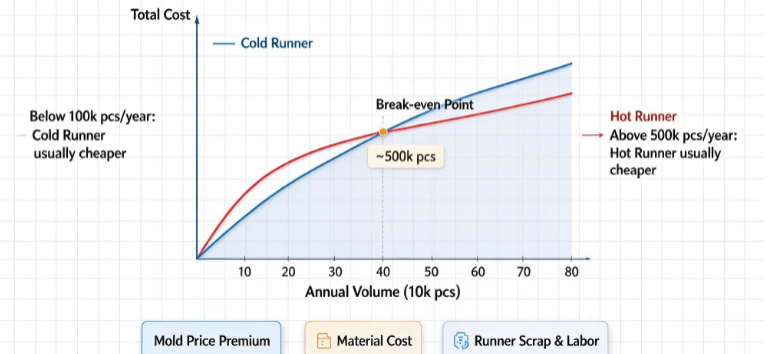
Example: Product weight 10g, cold runner scrap 8g, high-priced PC, runner reuse recovers only 50% of original value. When annual output exceeds 500,000 pieces, cumulative savings cover the hot runner price difference, and every piece after that is pure savings.
Hidden Cost Reminders:
High recycled material ratio leads to higher defect rates;
Grinding, sorting, handling, and storage occupy labor and space;
Cold runner cooling is limited by runner thickness — longer cycle, lower machine capacity.
✅ Choose Hot Runner:
Annual output ≥ 500,000 pieces, long-term stable orders
High-priced engineering plastics such as PC, POM, PEEK
Multi-cavity molds
High appearance requirements, tiny gate marks needed
Fully automated production desired
Long product life cycle
✅ Choose Cold Runner:
Annual output < 100,000 pieces, short life cycle orders
Frequent color or material changes
Budget priority on upfront mold investment
Cheap material, stable runner reuse
R&D trial molds, small-batch validation projects
❌ Large volume must choose hot runner — If frequent color changes, purging waste and downtime will offset the savings.
❌ Cold runner scrap grinding and reuse = no waste — Ground material performance declines and can only be blended back in proportion, with depreciation loss.
❌ Hot runner only saves material — It also shortens the molding cycle and improves machine output; this capacity benefit is often omitted.
The choice between cold and hot runners should not only look at the mold quotation, but at the total life cycle cost.
Small batch, short cycle, multiple color changes: cold runner upfront investment is controllable and reliable;
Large batch, long cycle, expensive raw materials: although the hot runner mold is more expensive, it saves material, labor, and improves capacity — after crossing the break-even line it continuously reduces costs.
In the early stage of the project, we can calculate the break-even output separately based on product weight, runner weight, material unit price, and estimated annual output, and provide the most economical runner solution.