Molds determine plastic product precision, appearance and long-term production efficiency. As a professional custom mold maker, Shenzhen JBRplas Technology Co., Ltd. (JBRplas) has developed a standardized full-process acceptance checklist covering all core mold sections to eliminate defects before delivery.
Founded in 1995, we are a family-owned manufacturer with a 10,000 m² factory, 30 injection machines and an in-house mold shop capable of over 45 molds monthly. ISO-certified and familiar with European quality norms, our plant is just 30 minutes from Shenzhen International Airport for efficient global shipment.
1. Mold Base & Appearance Check
All visual and structural standards ensure safe transport, installation and maintenance:
Engraved nameplates display mold ID, weight and dimensions; DATUM marks and component serial numbers are printed on every plate. All edges have ≥1.5mm chamfers.Cooling, air and oil nozzles are labeled IN/OUT with serial codes. Exposed cylinders and nozzles are protected by support legs.Parts heavier than 10kg are fitted with lifting eye holes for balanced hoisting. Mold surfaces are free of rust, pits and redundant holes.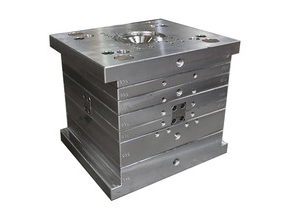
2. Ejection, Slide & Core-Pulling Performance Test
Smooth demolding avoids flash, sticking and mold collision during production:
Ejector pins, lifters and slides run without jamming or abnormal noise. Sliding parts are nitrided to HV700 with built-in oil grooves for wear resistance.Standard load-matched mold springs have 10%–15% pre-compression for full ejector reset.Slides and lifters are equipped with travel limiters; wide slides over 150mm adopt hardened wear plates. For interfering structures, forced pre-reset devices and travel switches are mandatory.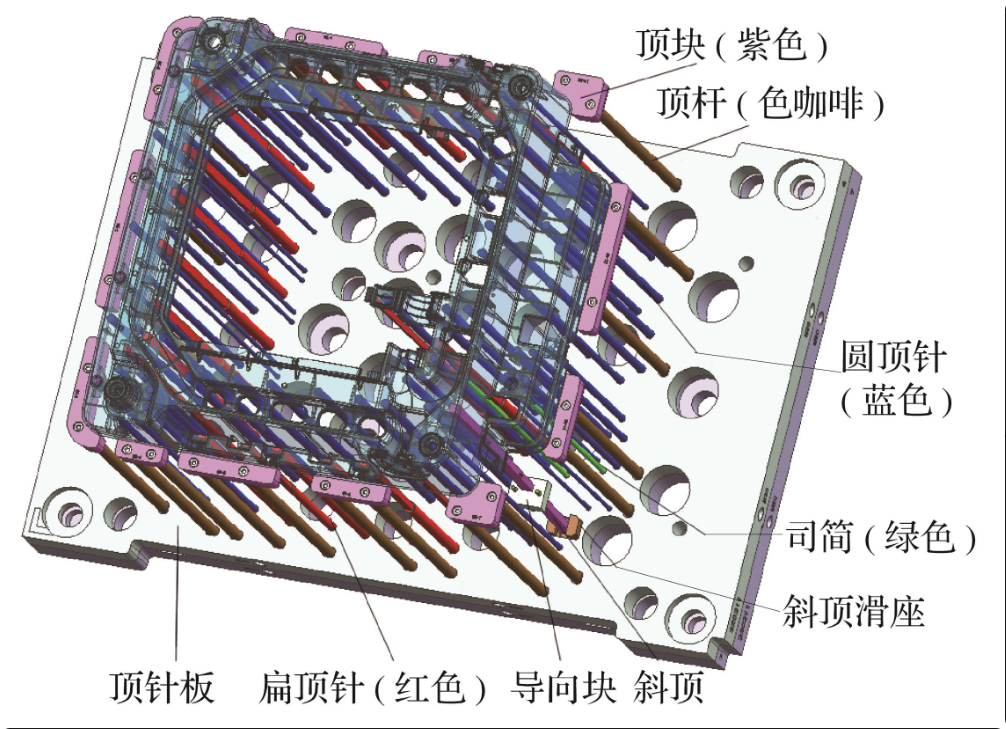
3. Cooling Circuit Leakage Test
Well-designed cooling shortens cycle time and reduces warpage:
Water channels follow drawing specs with unobstructed flow. All molds pass a 4MPa, 5-minute pressure leakage test before sampling.
Standard sealing grooves with grease-coated O-rings are applied; brass baffles prevent corrosion inside channels. All oil and air lines are cleaned to remove metal debris.
4. Standard Gating System Inspection
Gates and runners directly affect surface quality and material waste:
Sprue bush is polished to Ra1.6; sub-runners finish to Ra3.2, all CNC/EDM machined instead of hand-ground.Three-plate molds feature optimized trapezoidal runners and sprue pullers for easy runner stripping. Submarine gates are adjusted to eliminate sink marks on cosmetic surfaces.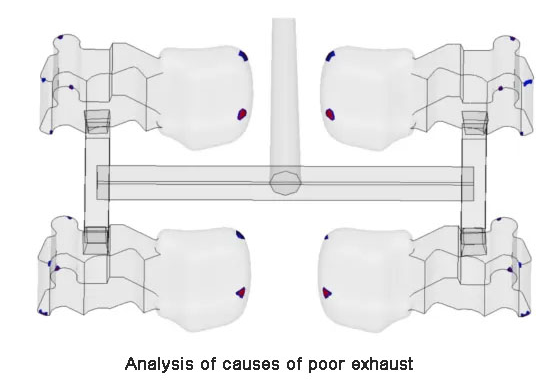
5. Cavity, Parting Line & Vent Inspection
This section guarantees dimensional accuracy and flawless appearance:
Cavity surfaces meet customer finish requirements (SPI mirror/fine finish, VDI matte texture), free of tool marks and EDM textures.
Parting lines are fully lapped with over 70% contact area; vent depth is controlled under plastic flash limits. Ribs deeper than 15mm use split inserts.
Draft angles are customized by material and texture: ≥3° for PS, ≥2° for ABS/PC, 3–5° for textured surfaces. Wall thickness tolerance is controlled within 0.05mm.
L/R marks, date codes and logos are engraved at agreed invisible positions; transparent mold inserts are mirror-polished. All shut-off structures adopt ≥2° draft to prevent sharp burrs.
6. Packaging, Spare Parts & Complete Technical Documents
We deliver full supporting materials alongside each mold:
Cavities are sprayed with anti-rust oil; moving parts coated with grease. At least two locking plates are installed for safe shipping.Complete vulnerable spare parts with supplier lists are attached.Full documents include 2D/3D drawings, cooling layout, material certificates, trial mold reports and operation guides. All raw materials, colorants and coatings comply with RoHS & REACH.
7. Trial Mold & Mass Production Qualification
Molds pass strict sampling verification before final acceptance:
Full dimension First Article Inspection (FAI) and formal trial reports are provided. Critical dimensions maintain CPK ≥1.33 for stable output.
Optimized injection parameters are recorded; molding yield ≥95% and coating yield ≥90%.
The first three production batches pass full appearance and dimensional tests matching approved samples.
About JBRplas
Established in 1995, JBRplas is a family-run precision mold and injection molding manufacturer. Our in-house mold workshop delivers over 45 sets monthly, fully complying with European quality standards.
Every mold undergoes cross-department inspection by mold, QC, engineering, purchasing and R&D teams before shipment. Our rigorous acceptance rules cut post-delivery maintenance costs and support stable mass production for consumer electronics, wearables, automotive and construction plastic parts worldwide.